Improving yield is not merely a production target. It protects material, labor, delivery schedules, and customer trust. In PCB manufacturing, one hidden defect can begin with a contaminated laminate surface, continue through drilling, and appear during final electrical testing. That delay makes the real cause harder to find.
IPC’s 2024 Electronics Industry Sentiment Report and Prismark’s 2024 PCB Industry Report show an industry facing cost pressure, supply uncertainty, and demanding technology requirements. These reports reinforce one practical point: stable processes matter as much as higher output. IPC-A-600 and IPC-6012 also provide essential acceptance and performance guidance for finished boards. However, standards cannot repair weak process control. Engineers still need clean data, disciplined inspections, and fast feedback from the production line.
So, how to improve yield rate in pcb manufacturing? The answer begins with measurable causes, not assumptions. Track defect types by layer, machine, shift, material lot, and operator. Inspect copper thickness, solder-mask alignment, drill accuracy, and etching results before defects multiply. Use statistical process control, automated optical inspection, and carefully designed root-cause reviews. Small details matter. A clogged drill bit can create hundreds of rejected panels.
Quality pioneer Dr. W. Edwards Deming stated, “Quality comes not from inspection, but from the improvement of the production process.” That principle remains powerful, although inspection still provides valuable evidence. No factory is perfectly stable. Yield improvement requires continuous learning, honest reporting, and occasional reconsideration of methods that once seemed reliable.
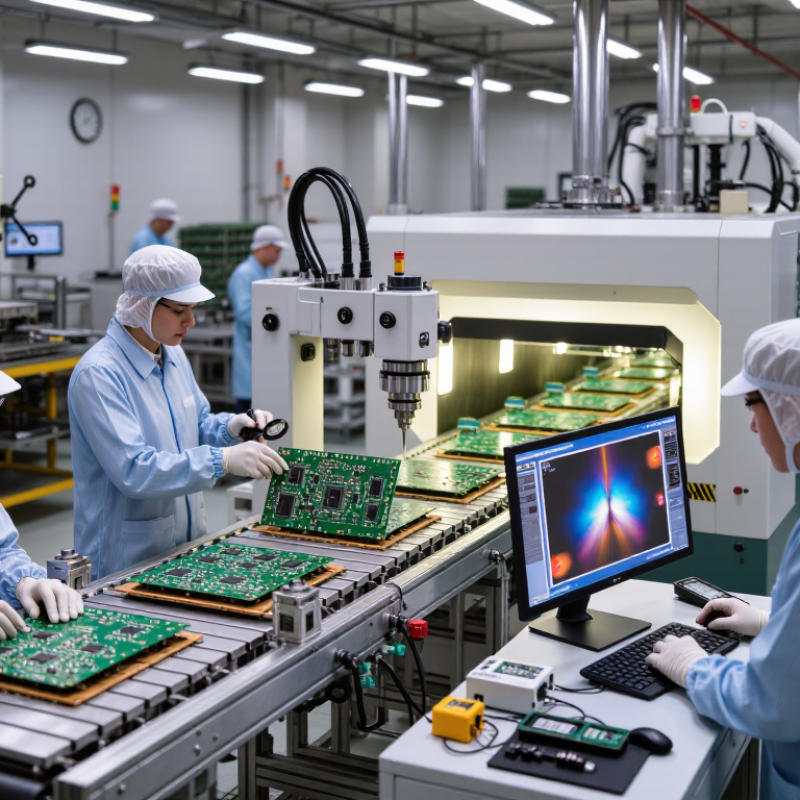
Yield improvement starts with definitions, not slogans. For each production lot, track first-pass yield (FPY), rolled throughput yield (RTY), and scrap rate. FPY measures boards passing inspection without repair. RTY multiplies pass rates across printing, drilling, imaging, plating, and assembly. Record the denominator clearly: panels loaded, boards tested, or shipped units. Mixed denominators create convincing, useless charts.
At the line, connect every failed board to a process step, defect code, machine setting, material batch, and operator shift. Pareto charts often expose a small group of losses, such as solder bridgingopen circuitsdrill breakout. Use optical inspection, electrical testing, and cross-section analysis to verify the suspected cause. Do not blame inspection alone. A false failure can hide a weak test fixture, while a missed defect can reach the customer.
In one review, our dashboard showed 96% yield, yet rework consumed hours each shift. Later, we separated repaired boards from true first-pass units and found the reported rate was overstated. That mistake mattered. Review yield by product, layer count, and process route, not only by factory average. Set a traceable defect hierarchy, audit data weekly, and challenge unusual improvements before celebrating them. Clean data is not automatic.
Standardize Design Rules for Manufacturability
Yield improvement often begins before layout starts. A shared design-rule library should define trace widths, spacing, drill sizes, copper weights, solder-mask clearances, and component keep-outs. These limits must match the selected fabrication process, not personal preference. IPC-2221 and IPC-7351 provide useful foundations, but they cannot replace supplier-specific capability data.
IPC’s 2023 PCB Technology Roadmap highlights tighter geometries, higher layer counts, and rising demand for high-density interconnects. These trends leave less room for informal decisions. A 0.10 mm spacing rule may pass inspection on one line but fail on another. The difference can appear beside a via, under a fine-pitch package, or near a copper pour. Define the rule in the CAD library, then verify it against current process capability.
Make the checks practical.
Manufacturing teams should review the rule set quarterly using defect Pareto charts, first-pass yield, and engineering-change records. The 2024 IPC Electronics Industry Survey identified supply-chain and manufacturing consistency as continuing industry concerns. That supports a controlled, documented workflow. Yet standardization can become rigid. We once treated a clearance table as permanent, then discovered it ignored a new surface-finish constraint. The rule was technically neat, but operationally wrong. Keep revision history, record exceptions, and require a manufacturability review before release. Small, repeatable rules usually outperform heroic corrections after fabrication.
Reference comparison of common PCB design-for-manufacturability controls before and after standardized design rules are applied. Values are production planning benchmarks and should be validated against the selected materials, fabrication process, and equipment capability.
| Design or Process Dimension | Common Baseline Condition | Standardized Manufacturability Rule | Reference Target | Expected Yield Effect | Control Method |
|---|---|---|---|---|---|
| Minimum trace and space | Mixed values across projects, including isolated features below the preferred process capability. | Use a controlled minimum trace and space value for each copper process and layer type; require engineering approval for exceptions. | At least 0.10 mm for capable fine-line processes; use a larger value when the process requires it. | Lower open and short defects | CAD rule check |
| Pad-to-copper clearance | Clearance varies by footprint library and may not account for etching, registration, and solder-mask tolerances. | Define pad, copper, and mask clearances in a controlled library and verify them against fabrication tolerances. | Use the fabricator-approved clearance for the selected technology; avoid unapproved exceptions. | Fewer shorts and mask slivers | Library governance |
| Annular ring | Small or inconsistent annular rings around drilled holes create breakout risk after drilling and registration variation. | Set a minimum finished annular ring and apply larger copper features where drill tolerance or aspect ratio is more demanding. | Typically 0.05–0.10 mm minimum, subject to the qualified drill and registration process. | Reduced breakout defects | Footprint validation |
| Finished hole size | Hole dimensions are specified without consistently accounting for plating, drill wear, and finished-size tolerance. | Specify finished hole size, tolerance, plating condition, and the corresponding drill compensation in the fabrication drawing. | Use the qualified hole tolerance for each hole class; separate plated and non-plated holes. | Better hole-size conformance | Drawing review |
| Drill aspect ratio | High depth-to-diameter ratios are used without checking plating coverage and drill capability. | Limit the finished-hole aspect ratio according to board thickness, hole type, material system, and qualified plating process. | Common through-hole planning limit: approximately 8:1 to 10:1, subject to process qualification. | Fewer barrel and plating failures | Stack-up review |
| Copper distribution | Large copper areas and sparse regions are distributed unevenly between layers or across the panel. | Balance copper density by layer and use copper thieving or pattern balancing where permitted by electrical requirements. | Maintain a consistent copper-density profile within the fabricator’s approved operating window. | Improved plating uniformity | Panel analysis |
| Thermal relief design | Thermal spokes differ between footprints, causing uneven solderability and heat transfer during assembly. | Standardize spoke count, width, and air-gap rules for power, signal, and thermal-sensitive connections. | Use library-controlled thermal patterns matched to copper weight and assembly process. | Fewer soldering-related defects | Footprint library |
| Solder-mask web and dam | Narrow or missing mask webs occur between closely spaced pads and vias. | Set a minimum mask-web rule and define when mask expansion, step-down, or mask removal is allowed. | Use the qualified mask capability; avoid relying on unsupported webs between fine-pitch pads. | Lower solder bridging risk | Mask DFM check |
| Via-in-pad usage | Via-in-pad is used without specifying filling, capping, planarization, or assembly requirements. | Restrict via-in-pad to approved applications and define filled-and-capped requirements when solder escape is possible. | Use only with documented fabrication and assembly capability. | Fewer voids and solder loss defects | Technology approval |
| Component-to-board edge clearance | Components, copper, or vias are placed too close to the routed edge or depanelization features. | Define separate keep-out zones for copper, plated holes, components, and sensitive features around the board outline. | Apply the approved edge-clearance value for the selected routing and assembly method. | Fewer edge damage and assembly defects | Outline validation |
| Panel utilization | Panel layouts prioritize quantity without sufficiently considering tooling rails, routing direction, coupons, and copper balance. | Use a standard panel template with defined rails, fiducials, coupons, spacing, and repeatable orientation rules. | Optimize utilization while preserving required tooling and process features. | Lower material and handling losses | Panelization review |
| DFM issue escape rate | Manufacturing issues are found late during quotation, tooling, or first-article review. | Run automated DFM checks before release and require closure of all critical violations before fabrication data approval. | 100% closure of critical DFM violations before release. | Higher first-pass yield | Release checklist |
| First-pass yield tracking | Yield is reported only at shipment or mixed with rework and repair results. | Track first-pass yield separately from final yield, classify defects by cause, and link recurring defects to rule updates. | Review yield and defect Pareto after every pilot and major design revision. | Continuous defect reduction | Quality dashboard |
Note: The target values are general engineering reference ranges rather than guarantees. Final design rules should be based on the selected material stack-up, copper weight, line technology, drill method, solder-mask process, panel construction, and formally qualified manufacturing capability.
Improving PCB yield begins with material control, not faster production. In my process reviews, moisture in laminate sheets often caused hidden delamination. Store materials in a stable, dry room, and record exposure time before processing. Confirm copper thickness, resin content, and shelf life before release. Small variations matter.
Equipment must hold repeatable conditions across every shift. Check drill runout, spindle vibration, imaging alignment, and plating current regularly. A simple maintenance log can reveal patterns that visual inspection misses. Calibration alone is not enough. Operators should compare actual readings with process limits during production. I once trusted a clean calibration report while ignoring inconsistent drill-wall quality. That delay increased scrap.
Production parameters need controlled experiments rather than guesswork. Adjust one variable at a time, such as etching temperature, conveyor speed, or press pressure. Track line width, hole quality, solderability, and warpage with measurable data. Use control charts to detect gradual drift before defects multiply. Keep approved settings visible near each workstation. Still, fixed recipes can become a weakness when materials or ambient conditions change. Review them after supplier changes, seasonal humidity shifts, or repeated nonconformities. Human judgment remains necessary, but it should be supported by records, samples, and clear acceptance criteria.
In-process inspection is more effective when it interrupts defects before they travel downstream. In one production review, solder bridges appeared repeatedly after reflow. Final testing caught them, but the real clues appeared earlier. Paste height varied near one edge, and the stencil opening showed gradual clogging. A simple setup check could have prevented hours of sorting. That lesson still matters.
Inspection should follow process risk, not just the production schedule. Operators can verify paste volume, component placement, drill quality, and copper pattern registration at defined intervals. Automated optical inspection helps locate missing parts, skewed components, and visible solder defects. X-ray inspection can reveal hidden voids or insufficient joints when the design requires it. Test coupons provide measurable evidence for plating thickness and hole reliability. Each result needs a clear reaction plan. Pause, contain, investigate.
Defect prevention improves when data connects to causes rather than sitting as isolated numbers. Track defect type, machine condition, material lot, operator, and time window. Use calibrated gauges and verify inspection systems with known samples. I would not treat every alarm as proof of failure. False calls waste attention, while missed defects damage trust. Reviewing both is necessary. Teams should challenge inspection limits when recurring defects pass unnoticed. That uncomfortable question may reveal a weak sampling plan or unclear ownership.
Yield rate improves when teams investigate causes, not symptoms. In PCB manufacturing, a failed board is evidence, not merely scrap. Root-cause analysis connects defects to process conditions, materials, equipment, and operator actions. I have found that the first visible fault often hides an earlier mistake. A solder bridge may begin with paste volume, stencil wear, or inaccurate placement. Measure before changing the line. Good records matter.
A practical analysis starts with a clear defect definition and a verified sample. Record board location, lot, machine settings, humidity, shift, and inspection results. Then compare good and failed boards using the same criteria. Use process maps, five-whys questioning, and controlled trials.
Do not accept “operator error” without evidence. That label can stop learning. One variable at a time. Small changes reveal more.
Corrective action should remove the cause and include a prevention check. Replacing a worn stencil is incomplete without a cleaning schedule and inspection limit. Track first-pass yield, defect type, and recurrence across several production runs. Review the data with production, engineering, and quality personnel.
Document failed experiments, too. They prevent repeated guesses. Root-cause analysis is not always clean. Some causes interact, and early conclusions can be wrong. Recheck them.
Store laminate sheets in a stable, dry room. Record exposure time before processing. Moisture can cause hidden delamination.
Confirm copper thickness, resin content, and shelf life. Small variations matter. I once underestimated minor material differences.
Check drill runout, spindle vibration, imaging alignment, and plating current regularly. Compare actual readings with process limits.
A simple log can reveal repeated problems across shifts. It may expose patterns that visual inspection misses.
Change one variable at a time, such as etching temperature or press pressure. Track line width, hole quality, solderability, and warpage.
Not always. Review settings after material changes, seasonal humidity shifts, or repeated defects. Fixed recipes can become weaknesses.
Record the defect location, material lot, machine settings, humidity, shift, and inspection results. Compare good and failed boards equally.
Do not accept “operator error” without evidence. Check materials, equipment, settings, and work conditions first. Measure before changing.
Remove the cause and add a prevention check. For a worn stencil, define cleaning intervals and inspection limits.
Track first-pass yield, defect type, and recurrence across several production runs. Document failed experiments too. They prevent repeated guesses.
Improving PCB manufacturing yield begins with clear, measurable yield metrics and a detailed understanding of where losses occur. By tracking defects across design, material preparation, assembly, testing, and rework, manufacturers can identify recurring problems and prioritize corrective actions. Standardized design-for-manufacturability rules also help reduce layout-related risks, improve process consistency, and prevent avoidable production difficulties before fabrication begins.
A practical approach to how to improve yield rate in pcb manufacturing also requires careful optimization of materials, equipment settings, and production parameters. Consistent in-process inspection can detect defects early, while preventive controls reduce the chance of repeated failures. When problems arise, structured root-cause analysis should be used to distinguish symptoms from underlying causes. Reviewing process data, verifying corrective actions, and continuously updating work standards creates a disciplined improvement cycle that supports higher yield, more stable production, lower waste, and reliable PCB quality.
Focus Laser